Copyright © 2026 Fluent Conveyors, LLC. All rights reserved.
The Fluent Conveyors logo is a registered trademark of Fluent Conveyors, LLC. Serial Number 97664258 Registered on Dec. 12, 2023


Copyright © 2026 Fluent Conveyors, LLC. All rights reserved.
The Fluent Conveyors logo is a registered trademark of Fluent Conveyors, LLC. Serial Number 97664258 Registered on Dec. 12, 2023
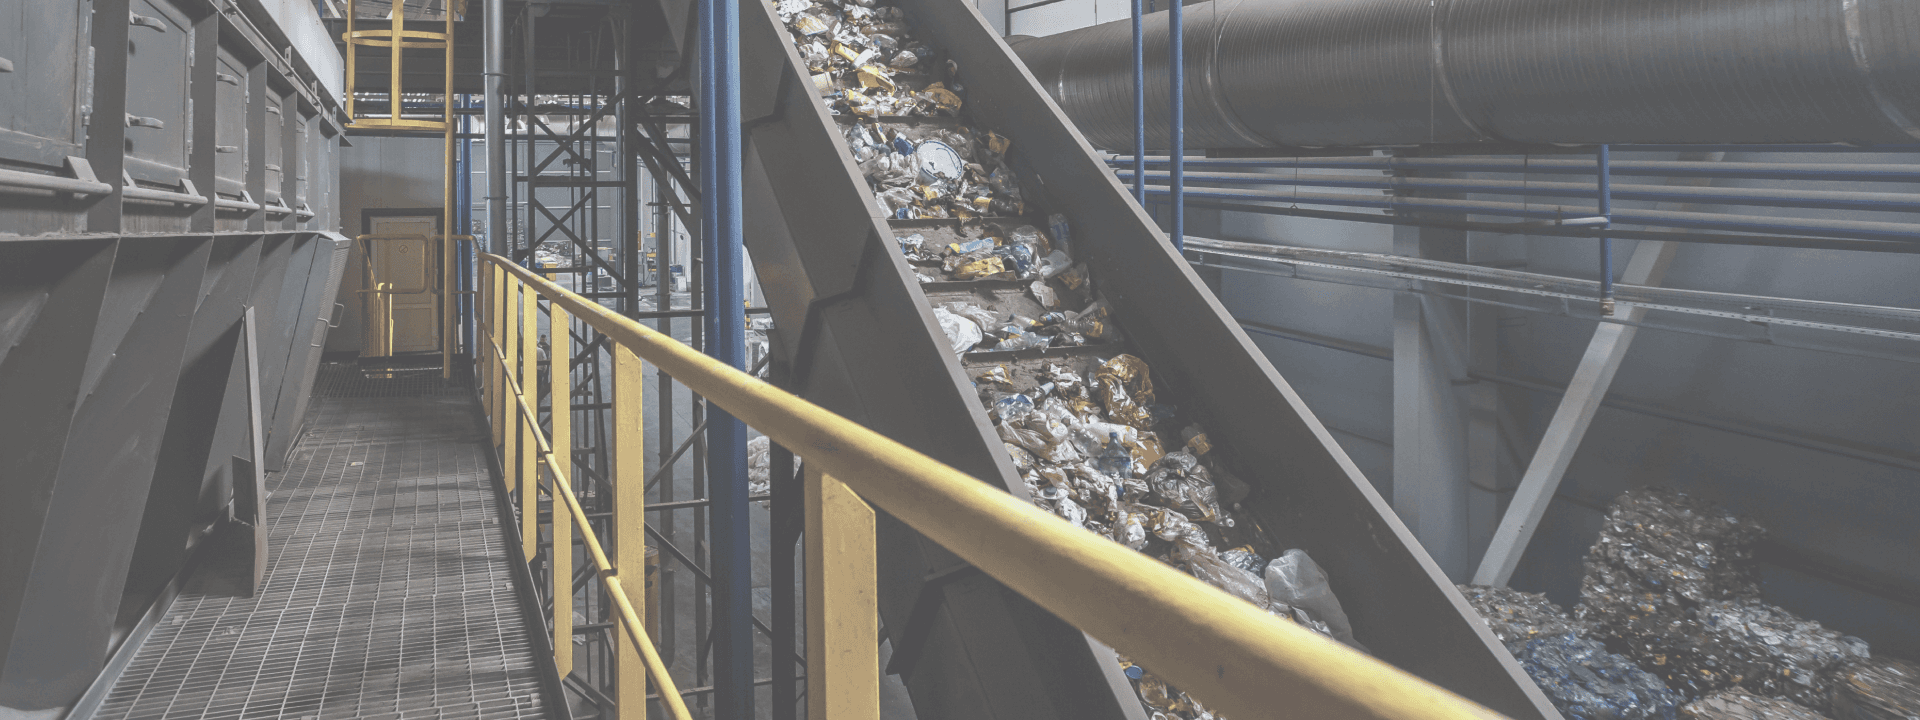
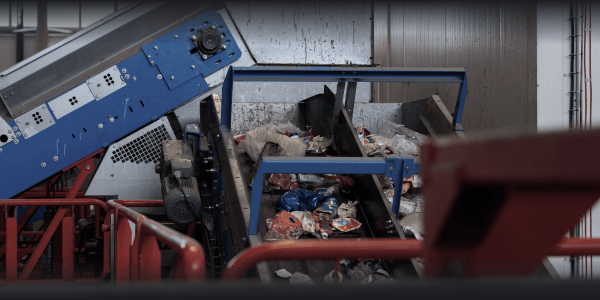
Mixed solid waste includes unsorted trash from municipal and commercial sources. It includes sharp scrap metal, oily organic matter, and household chemical cleaners. Waste management and material recovery facilities require conveyors that withstand heavy loads of mixed waste, and belts that resist abrasion, oils, and chemicals.

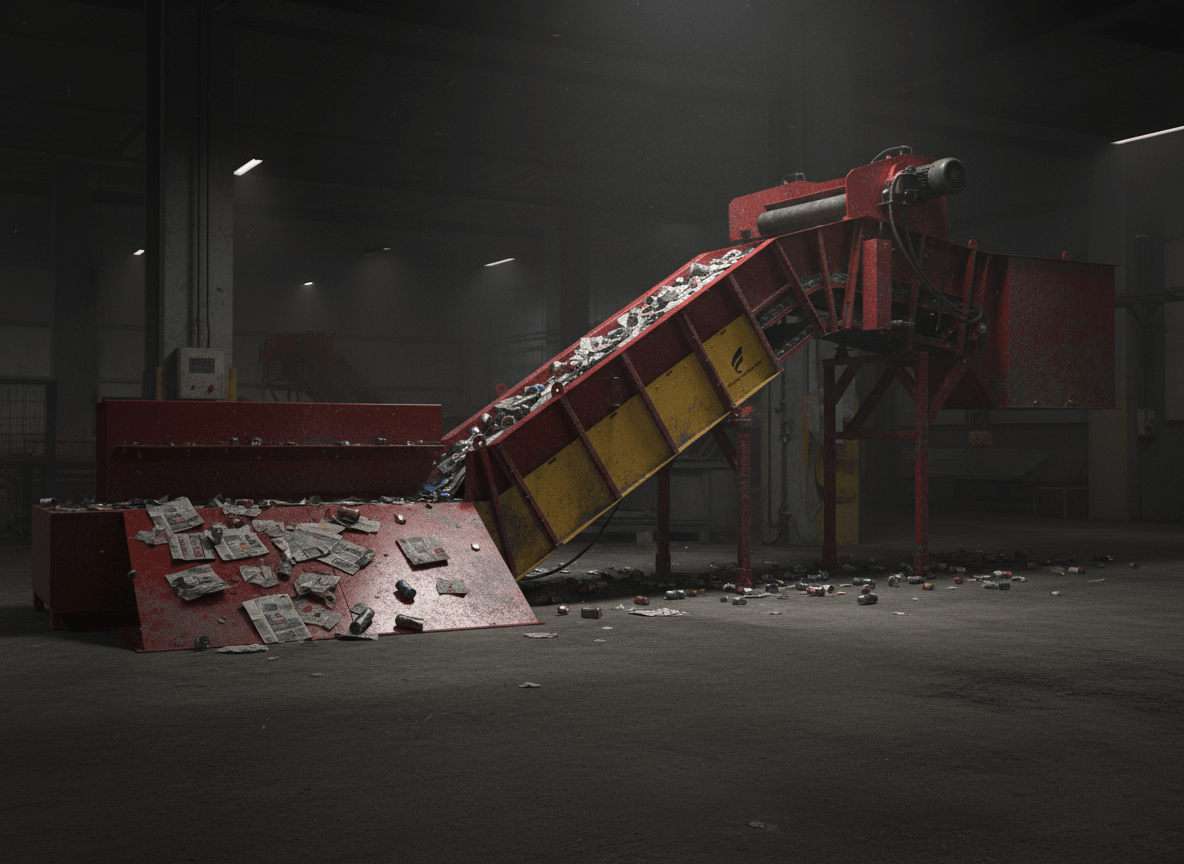
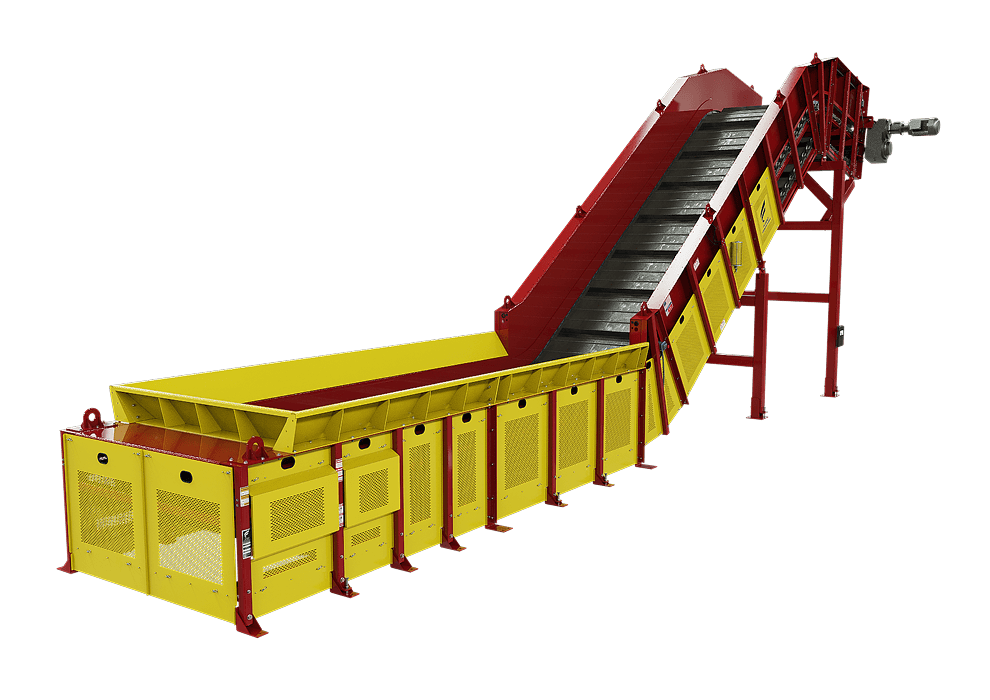
Roller chain conveyors are the preferred choice for many waste management operations because of their high torque, rugged construction, and versatile belt options. Roller chain conveyors are some of the best mixed waste conveyors on the market.
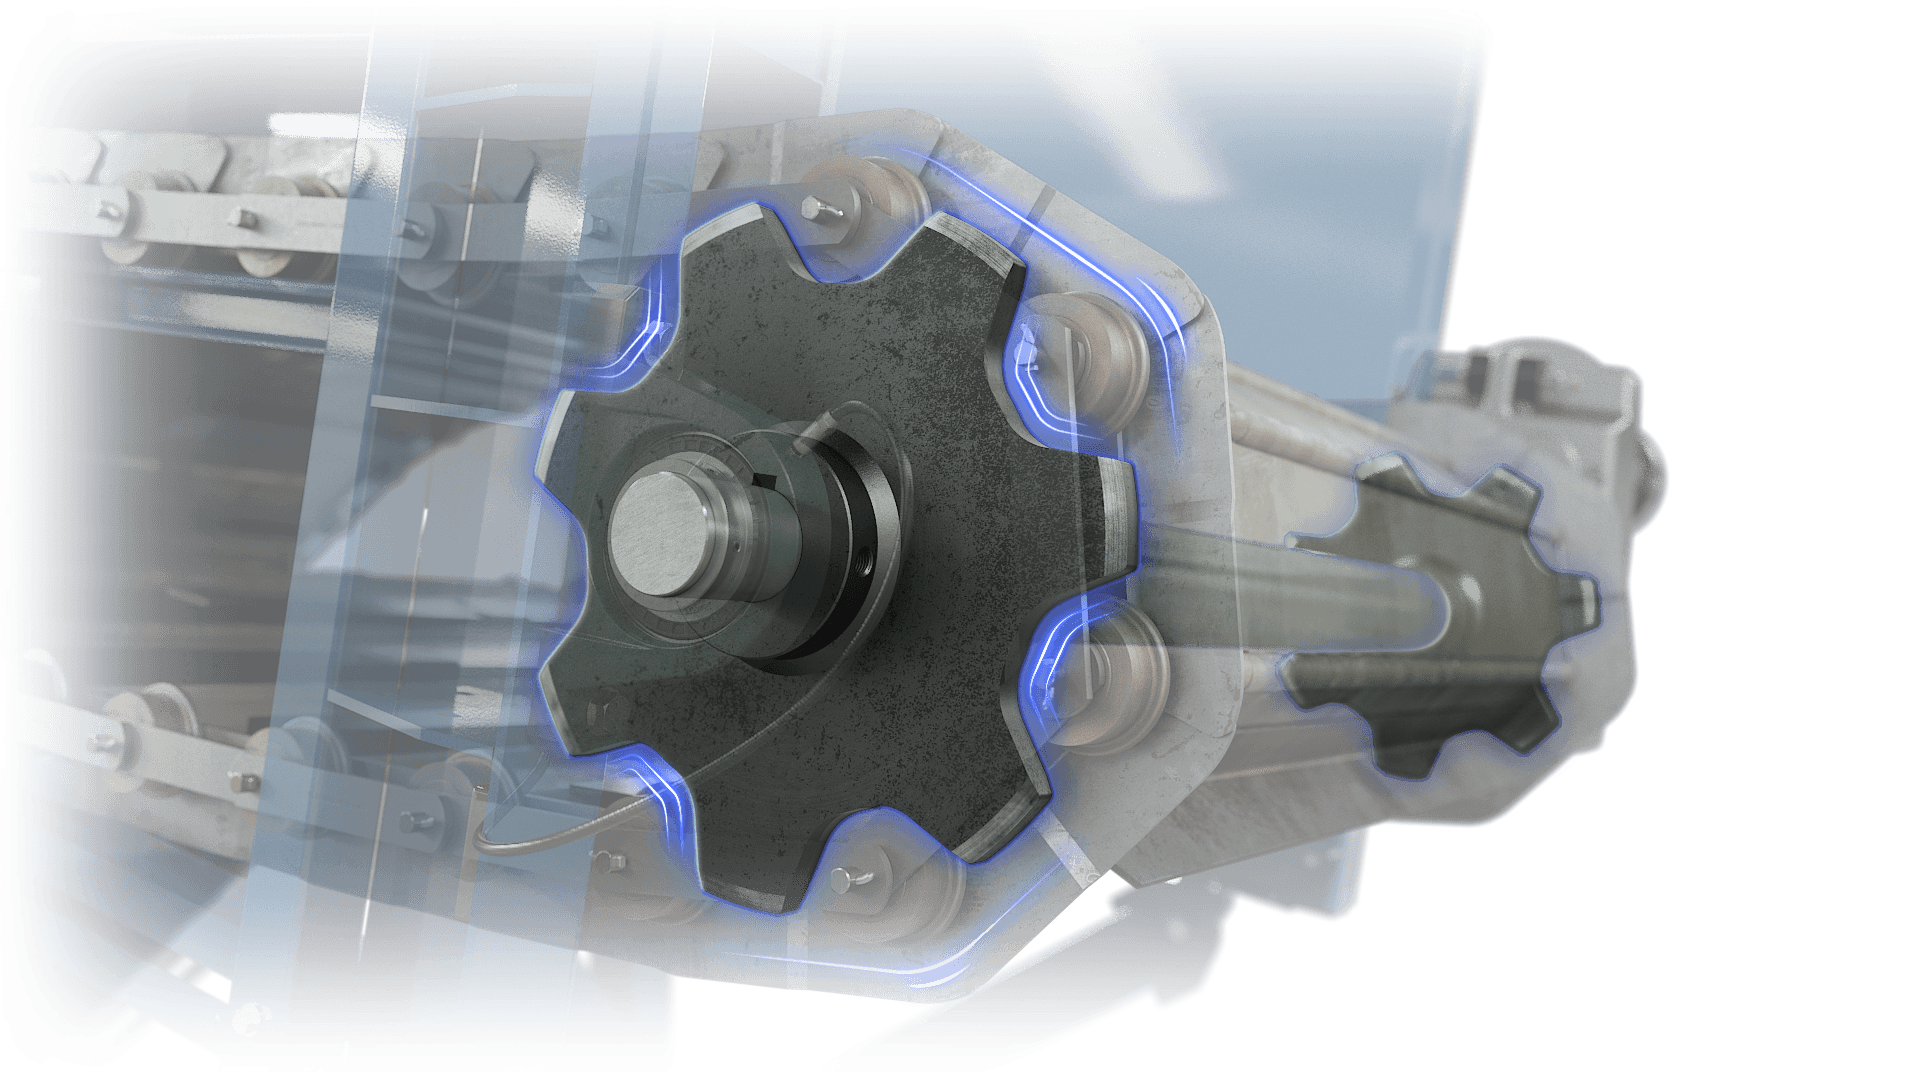
Unlike other conveyor types which are driven by a pulley, roller chain conveyors are sprocket-driven. The sprocket gives the conveyor more torque for handling abrasive and heavy materials.
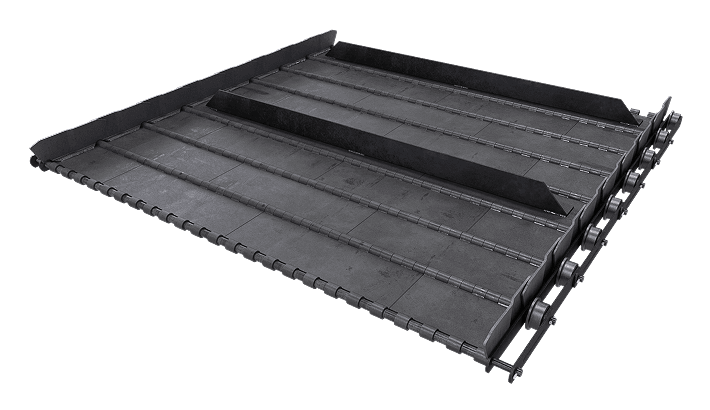
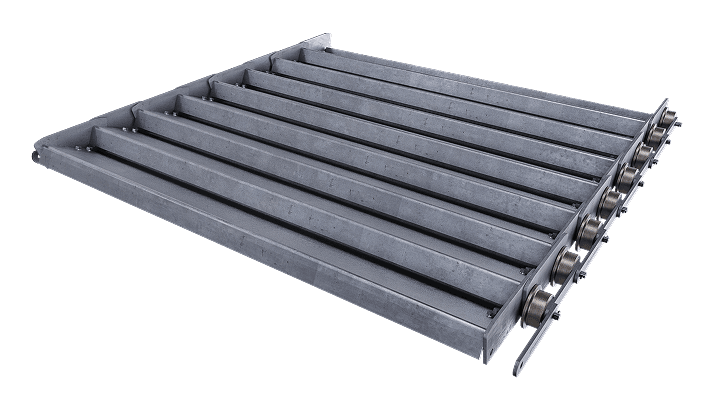
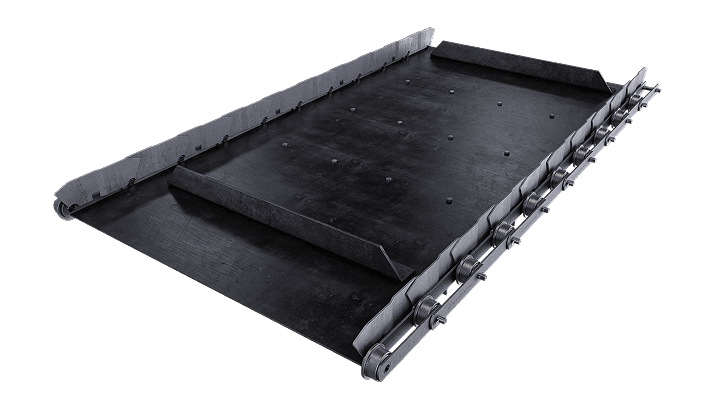
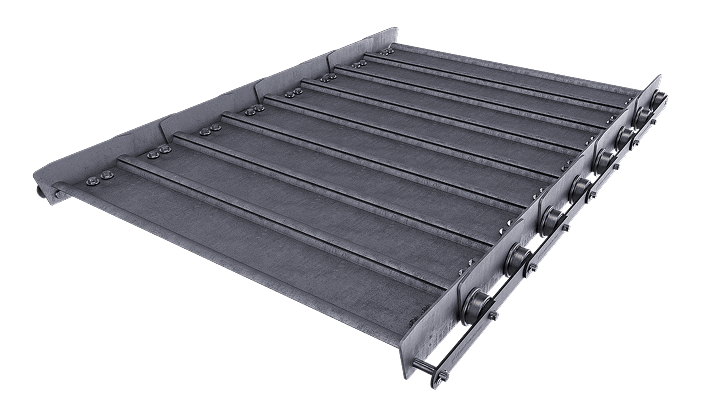
Modular, metal roller chain belts are tailored to specific application requirements. Different roller chain belts excel at handling different types of waste:
Are made with overlapping stainless steel plates, providing a strong conveying surface for large, heavy, or abrasive waste. They are best for bulk waste and sorted paper and cardboard.
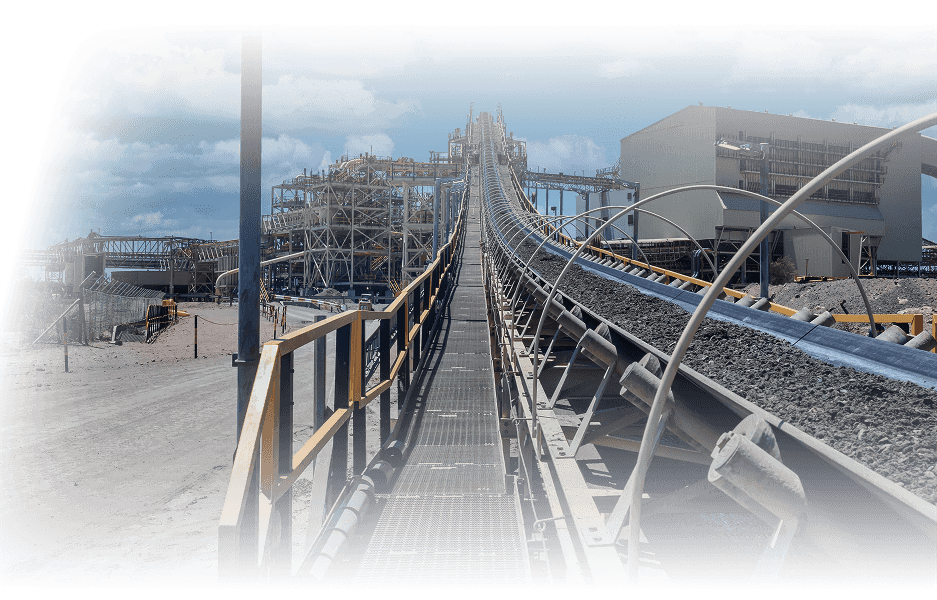
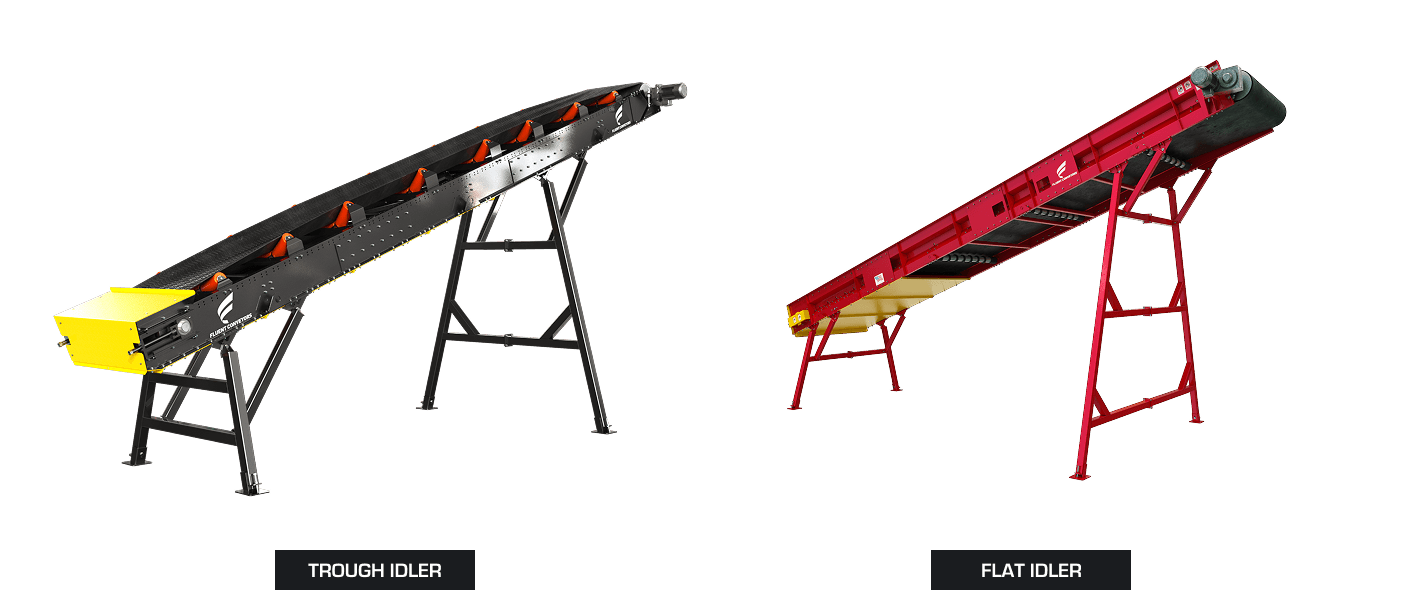
Flat idler and trough idler conveyors are common in waste management. They are pulley-driven belt conveyors that can be equipped with cleated belts to contain loose materials on inclines and declines.
Trough idler conveyors collect loose bulk trash at the center of the belt. They are best for organic waste. Flat idler conveyors more commonly transfer sorted waste and recyclables between screens, shredders, and other equipment.
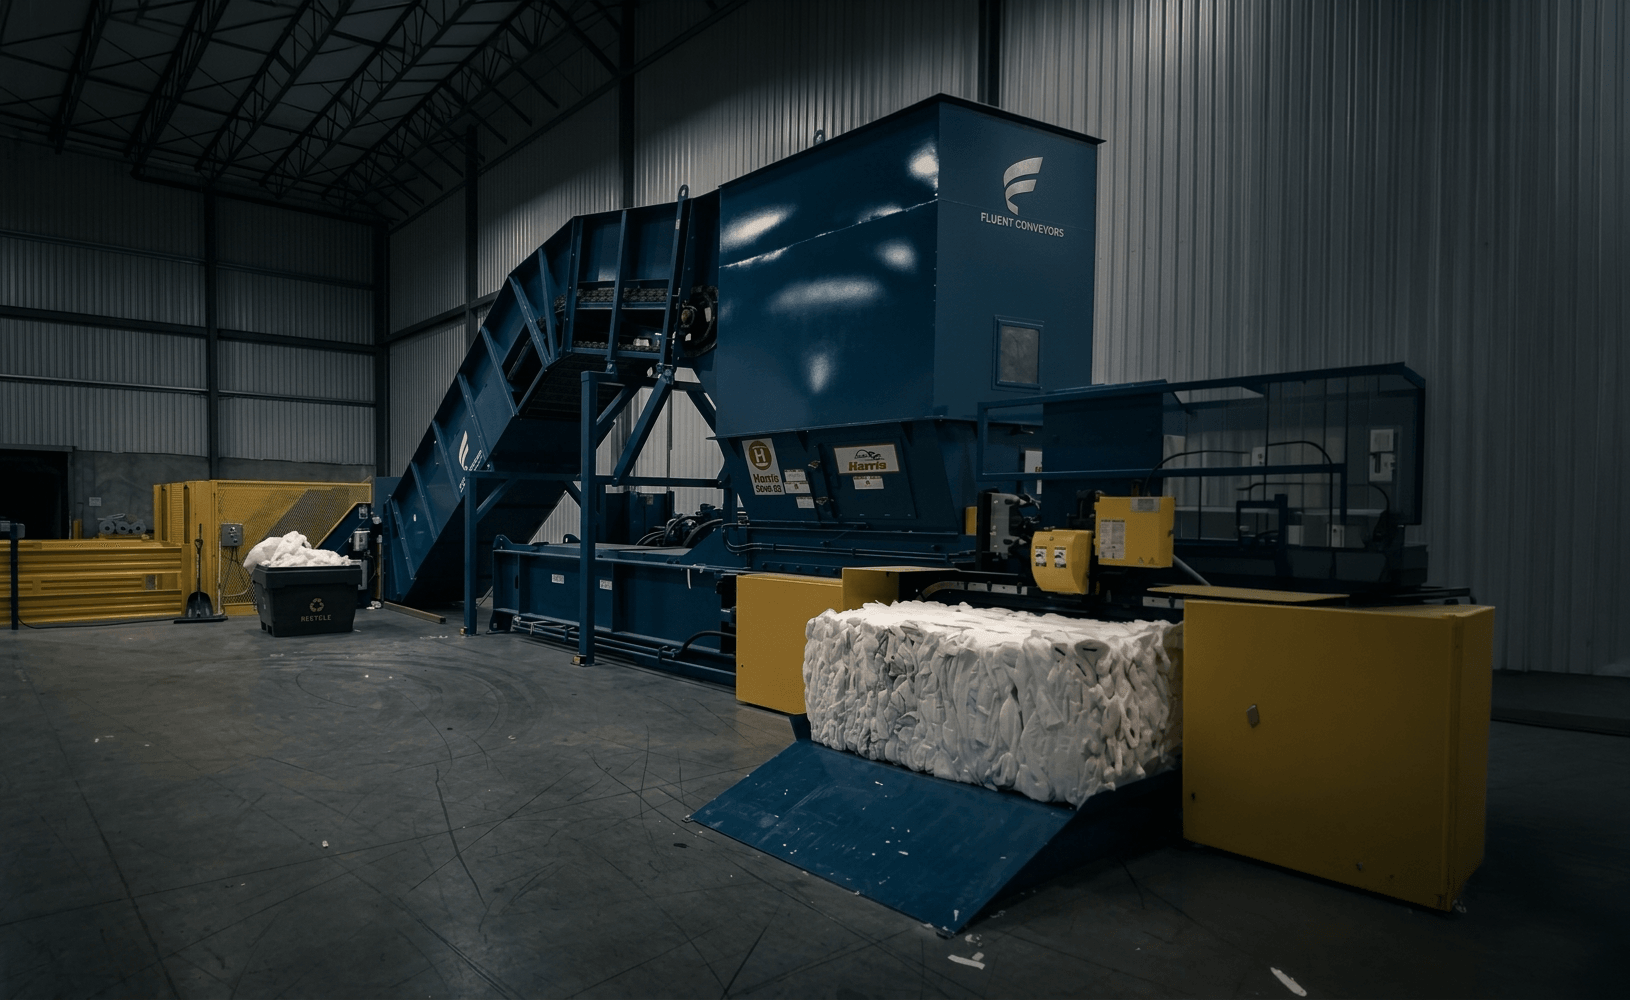
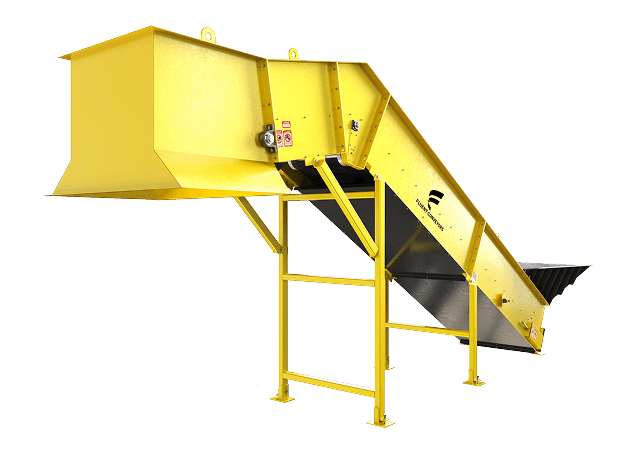
Slider bed conveyors can handle lighter waste, such as cardboard and plastics. Unlike with idler conveyors, the belt is supported by a smooth metal bed. This simple construction makes slider beds cost-effective and easy to maintain. They act as transfer, feed, and discharge conveyors that handle lighter waste.
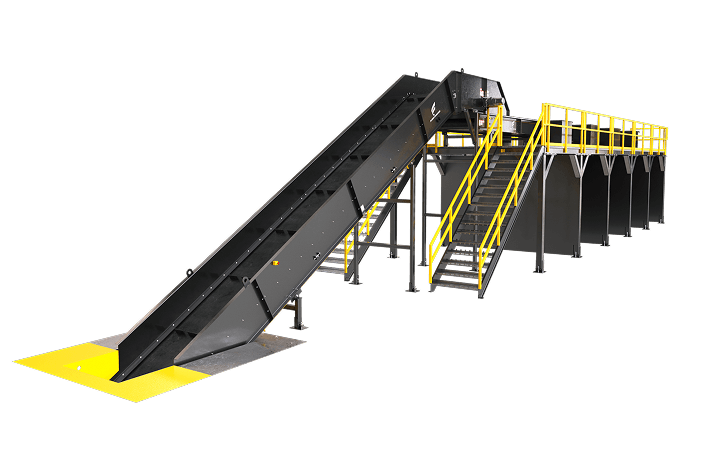
Recycling sort systems allow teams to sort valuable materials from mixed waste. They can be enhanced with chutes, diverters, and screens to process specific materials and mesh with other recycling equipment.
Conveyors perform the following tasks in mixed waste facilities:
We design and build conveyors for all industries and applications.
Are you looking for a custom conveyor solution? Let us help you design a conveyor that meets your needs. All Fluent conveyors are engineered and American made to meet the most stringent tolerances.

Goodyear, Flexco belt options resistant to rips, tears, and impacts

Baldor, Leeson, Toshiba TEFC motors selected for 24/7 operation

All systems fabricated by certified welders for structural integrity.

Formed using heavy duty steel plate, rectangular tubing, and structural channel

Precision components such as cold-rolled steel shafts and flame-hardened sprockets

All hardware is grade 8 for maximum strength

Extensively tested and inspected prior to shipment

3/16" and 1/4" thick structural steel frames to prevent flexing

25-35 pound rail track to withstand heavy loads

Designed for simple maintenance access and component serviceability

Dodge, Nord, SEW drives matched to application torque

ASTM A36 steel for fabrication per structural code

Premium bearings sized for L10 life ratings, made in USA

Painted with industrial-grade powder coating for durability
Made from premium components, our conveyors deliver exceptional strength and longevity. Whether you need a roller chain conveyor, a flat idler, or any other conveyor system, contact Fluent and tell us what you need. We will build you a custom conveyor—and you can even pick your own color.