Copyright © 2026 Fluent Conveyors, LLC. All rights reserved.
The Fluent Conveyors logo is a registered trademark of Fluent Conveyors, LLC. Serial Number 97664258 Registered on Dec. 12, 2023


Copyright © 2026 Fluent Conveyors, LLC. All rights reserved.
The Fluent Conveyors logo is a registered trademark of Fluent Conveyors, LLC. Serial Number 97664258 Registered on Dec. 12, 2023
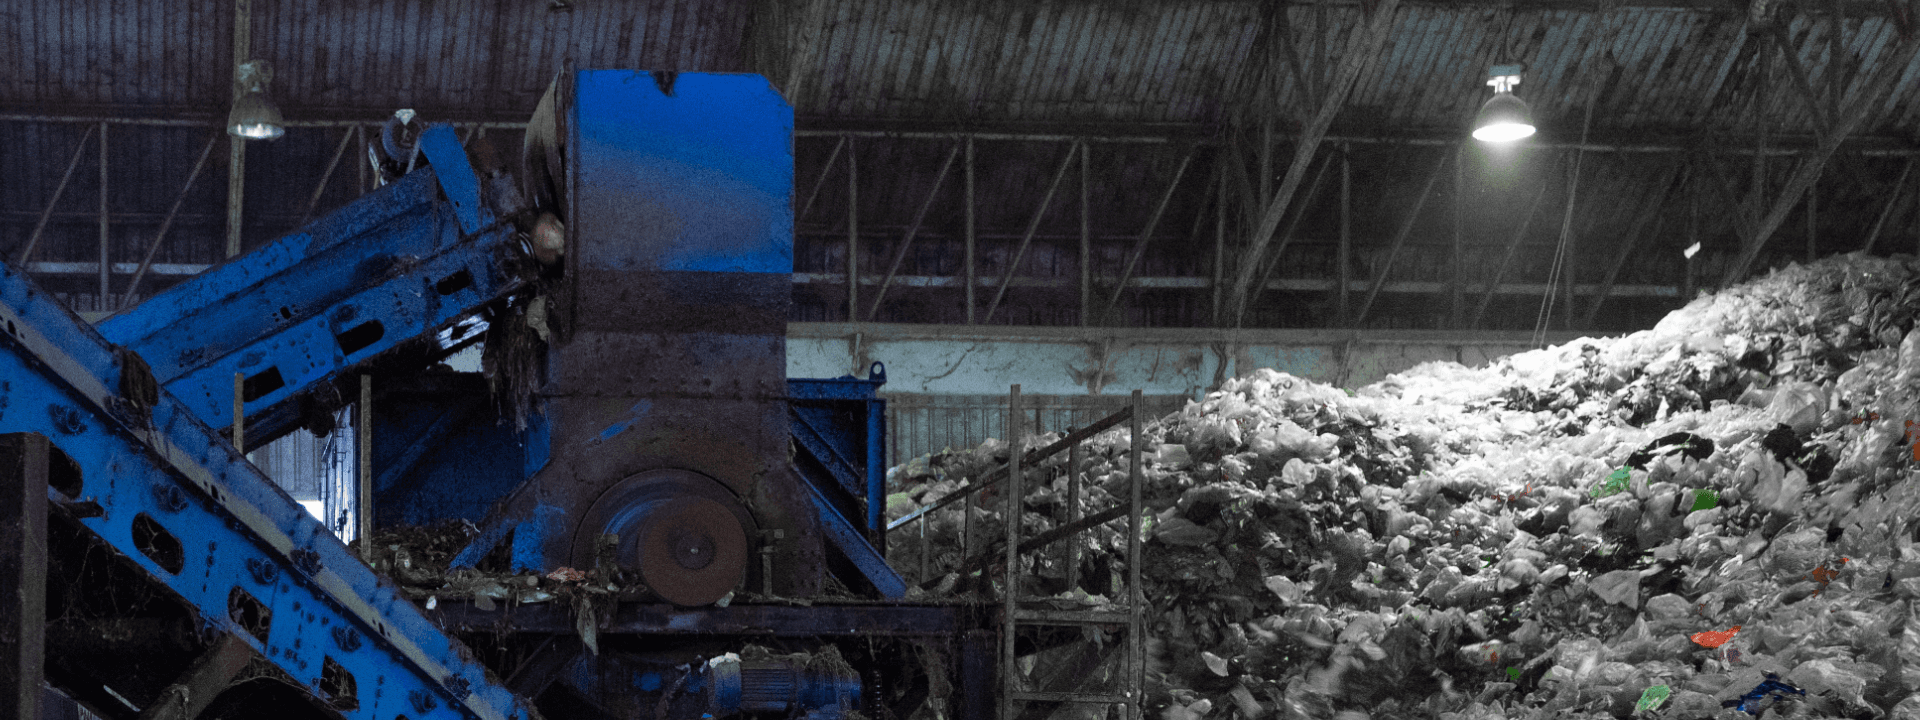
The best conveyors for recycling mixed solid waste are heavy-duty roller chain conveyors that take bulky, abrasive, contaminated feed off the tipping floor and meter it forward without jamming, with flat idler and slider bed conveyors moving lighter sorted fractions between screening, separation, and sorting.

Heavy-duty roller chain conveyors handle mixed waste, while slider bed conveyors move sorted materials.
Fluent designs and manufactures conveyors and conveyor systems for MSW recycling lines, made in the USA and built to drop into your plant layout.
An MSW recycling operation processes bagged household and commercial waste, bulky items, mixed material recovered from single-stream and MRF residue, and a shredded fraction that ranges from coarse pieces down to fines. Each stream arrives with its own size, moisture, and contamination load, and most of it passes through several conveyors before and after sorting.
Fluent builds the conveyors that move waste into, through, and out of the recycling line. That covers infeed off a tipping floor or receiving bunker, the metering conveyors that feed bag openers, shredders, and screens at a controlled rate, transport between screens, magnets, and separators, the conveyors that present an even layer to optical sorters, the discharge conveyors that carry rejects and recovered fractions clear, and the sorting conveyors that stage material for a manual pass.
If your line moves waste from a tipping floor to a screen, from a screen to a sorter, or from a sorter to a baler, contact us.
An MSW recycling plant is a sequence of equipment. Each conveyor is chosen for the material it carries and where it sits in the process. Six factors set the specification:
Below, we map conveyor types to their place in an MSW recycling line, explain why feed presentation drives both throughput and sorting accuracy, and detail the belt, liner, and drive choices that hold up through bulky, sharp, contaminated waste.
Material moves from receiving and infeed, through metering and size reduction, into screening, metal separation, optical sorting, and a manual QC pass before baling or storage. Let's look at the conveyors a typical plant might utilize at each point.

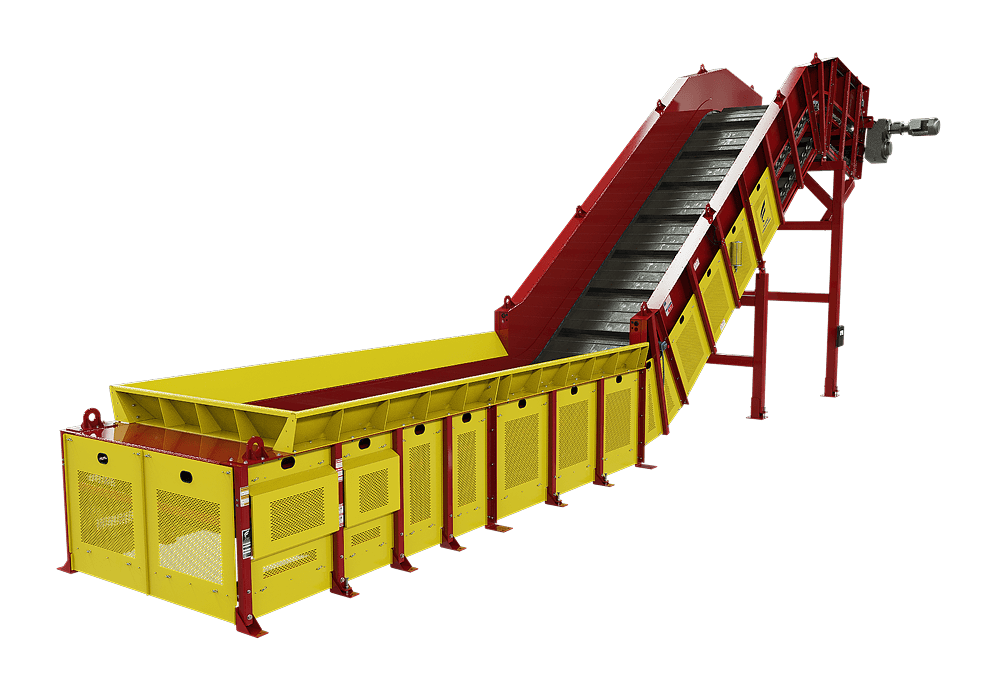
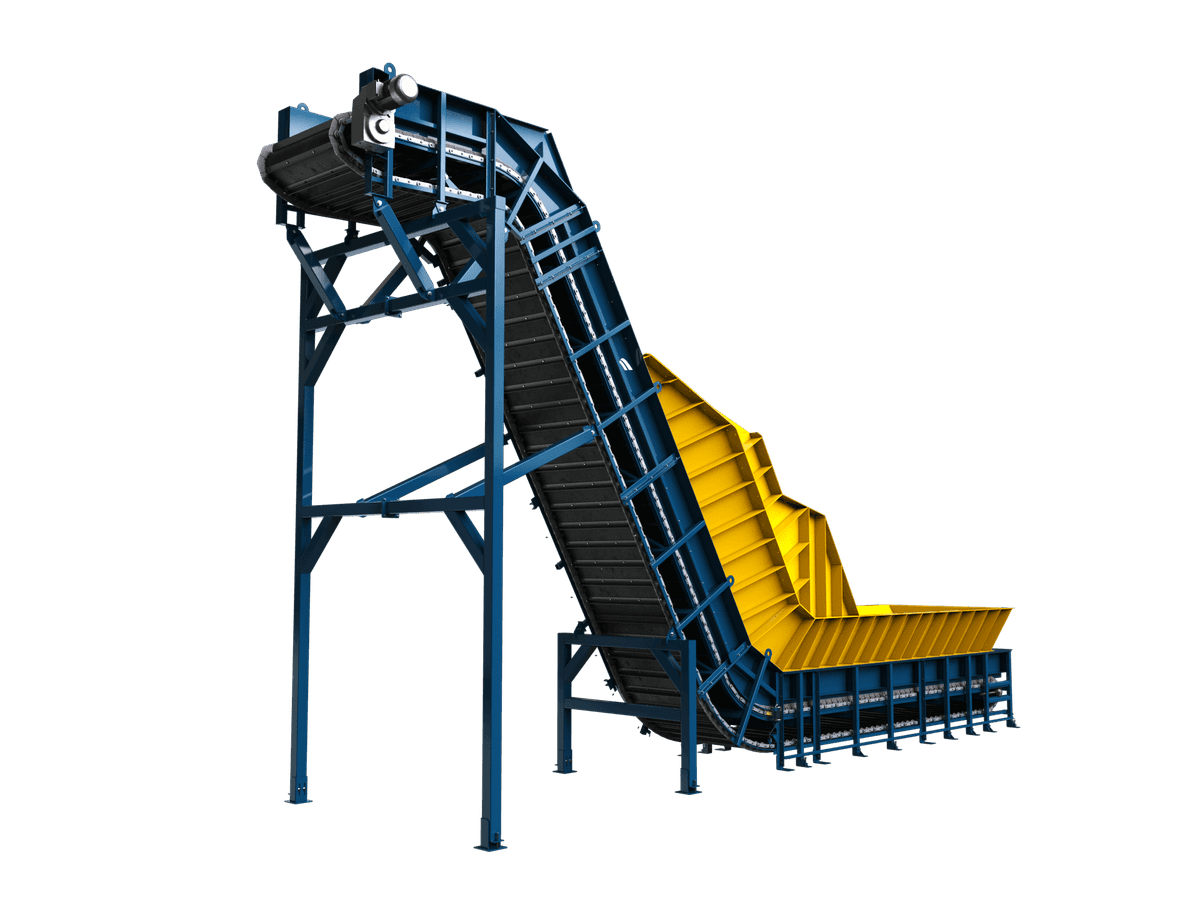
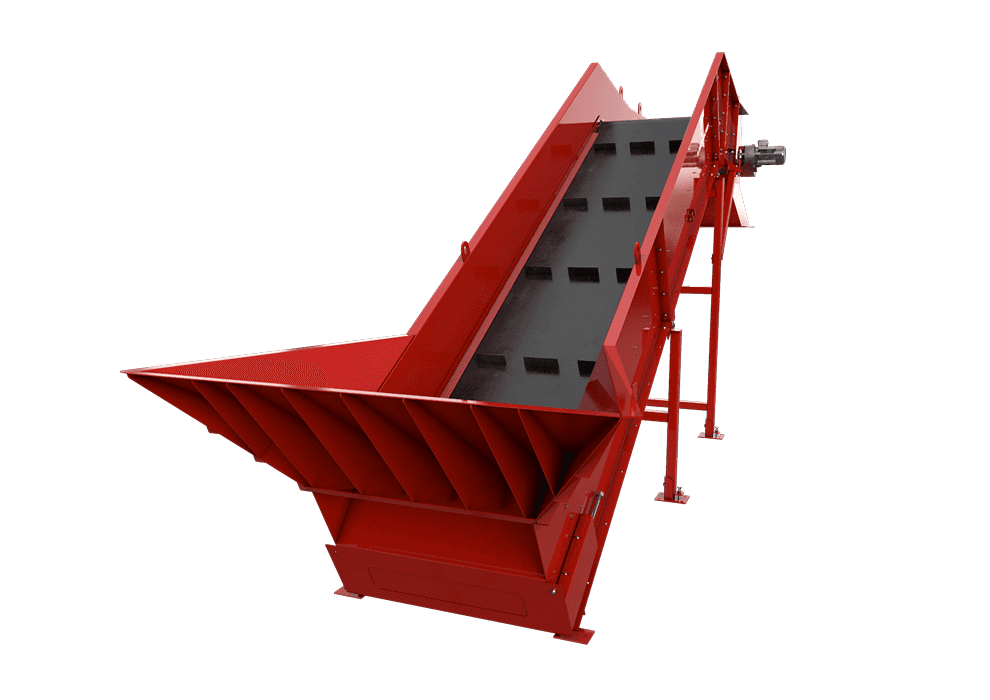
Bagged and bulky waste moves from the tipping floor or a receiving bunker toward metering and sorting. Roller chain conveyors with hinged steel or apron-pan belts take the weight of material dropped by a loader and feed it forward at a controlled, even rate, holding up to the metal, glass, and bulky items in the stream.
Waste is metered into bag openers, shredders, and screens on a feed conveyor, often with variable speed so the line can match feed rate to equipment capacity. A steady feed keeps each machine loaded without surging or jamming.
Where the line reduces waste for RDF or downstream sizing, tumble-back conveyors meter it into a shredder or hammer mill at a set rate and incline. This is one of two conveyors that decide how cleanly the line runs, while the other presents material to the optical sorters, covered below.
Oversize items, prohibited material, and non-target debris come out of the stream before and during processing. A recycling sort station gives workers a controlled area to pull large contaminants by hand, a magnet over the belt lifts ferrous metal, and an eddy current separator throws non-ferrous metal clear, all of which protect downstream equipment and clean up the recovered fractions.
Loosened and metered material crosses the plant to trommels, disc or ballistic screens, magnets, and separators. Roller chain conveyors carry heavier and mixed fractions over these runs, and flat idler conveyors move lighter, size-separated material at a stable speed between machines.
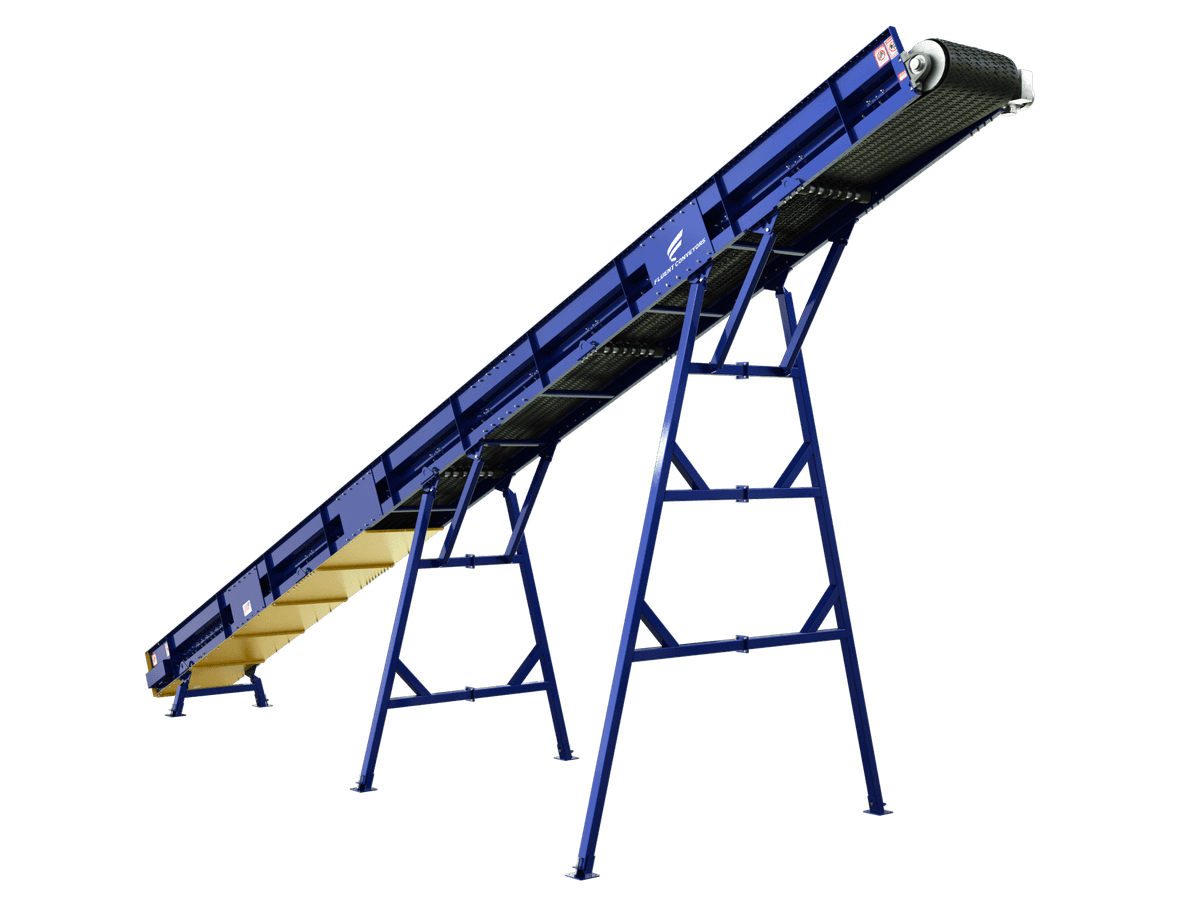
Sorted and separated fractions drop off screens and separators and move on to further sorting, baling, or storage. Flat idler conveyors carry an even burden between machines, and slider bed conveyors (a low-cost option for light, post-sort streams) handle the short transfers that move fractions through downstream equipment.
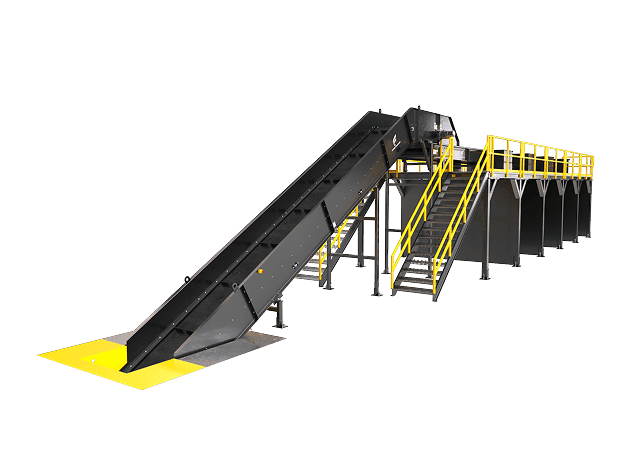
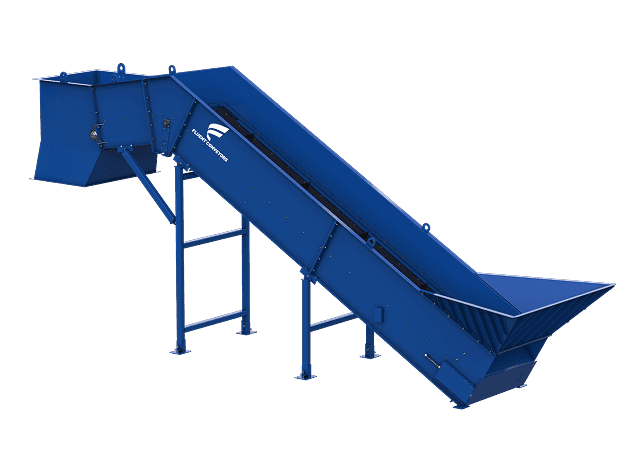
Recovered fractions often have to climb to an elevated screen deck, sorter, storage bunker, or baler infeed. Cleated belt conveyors carry material up these runs, with raised cleats holding it against rollback on the incline.
Recovered material moves on to a final sorting pass that refines each stream and removes residual contaminants. Flat idler conveyors present material as a stable, single layer for optical sorters and pickers to read, and recycling sort stations put workers on the line for the manual pass that cleans the stream before baling or storage.
The conveyor metering the front of the line sets the throughput ceiling, and the conveyor feeding the optical sorters sets how accurately the line separates material and pulls contaminants.
Four feed variables have the greatest effect on throughput and sorting accuracy:
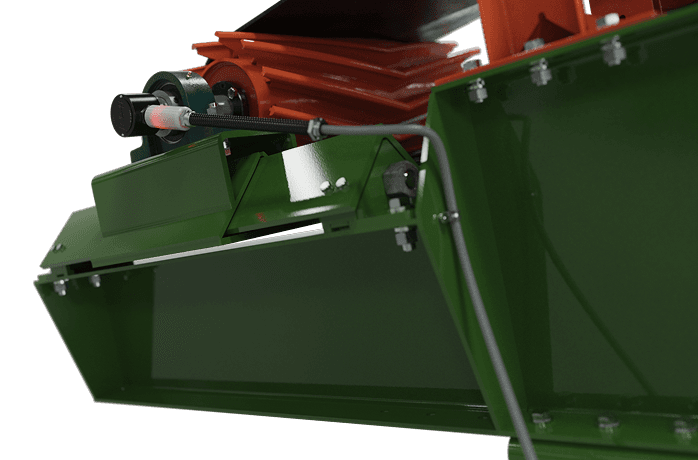
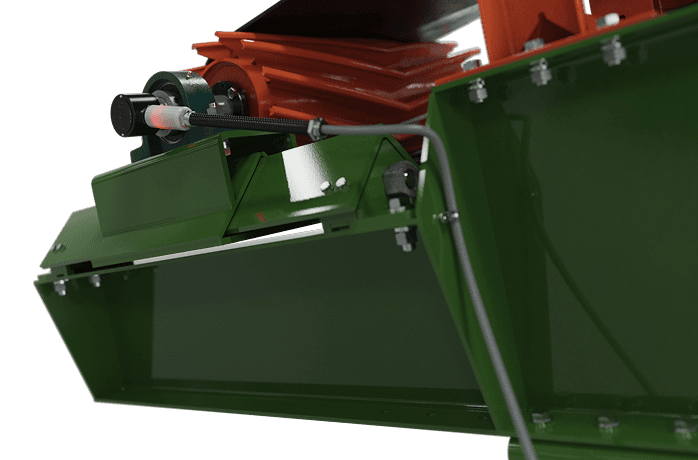
A speed sensor on the feed conveyor confirms the belt is holding the set speed under load, which keeps feed rate matched to equipment capacity and keeps the optical sorter's timing accurate.
Bulky, sharp, contaminated waste needs application-specific belts and conveyor add-ons. Fluent specs the carrying surface to the stream and stocks conveyor belts for MSW recycling.
Routine inspection and maintenance catch these early. Learn what causes wear and tear on a conveyor belt.
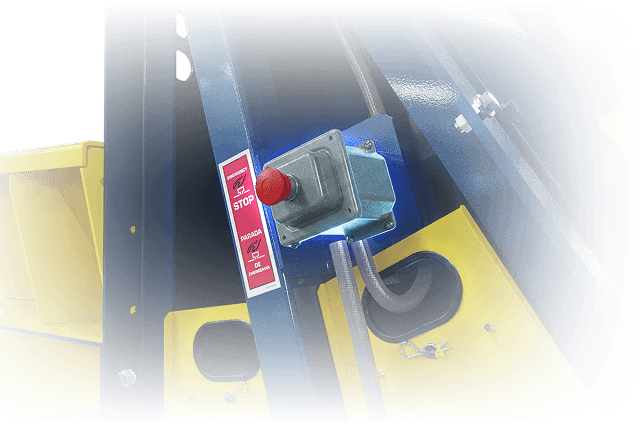
MSW recycling conveyors carry the hazards of moving belts, pinch points at pulleys and sprockets, exposed drives, and falling material, alongside hazards specific to mixed waste. Guarding, emergency stops, and pull cords are standard, and lockout/tagout access must be engineered for the frequent cleanout that jams, wraps, and spillage require.
Every conveyor in a recycling operation should exceed the safety standards imposed by the relevant authority. See how to reduce conveyor hazards for the details.
Fluent designs and builds custom conveyors and conveyor systems for MSW recycling lines.
Contact us to talk through your line, or send the material type, target capacity, and run dimensions, and our engineering team will scope a system to fit your plant and the rest of your MSW recycling line.