Copyright © 2026 Fluent Conveyors, LLC. All rights reserved.
The Fluent Conveyors logo is a registered trademark of Fluent Conveyors, LLC. Serial Number 97664258 Registered on Dec. 12, 2023


Copyright © 2026 Fluent Conveyors, LLC. All rights reserved.
The Fluent Conveyors logo is a registered trademark of Fluent Conveyors, LLC. Serial Number 97664258 Registered on Dec. 12, 2023
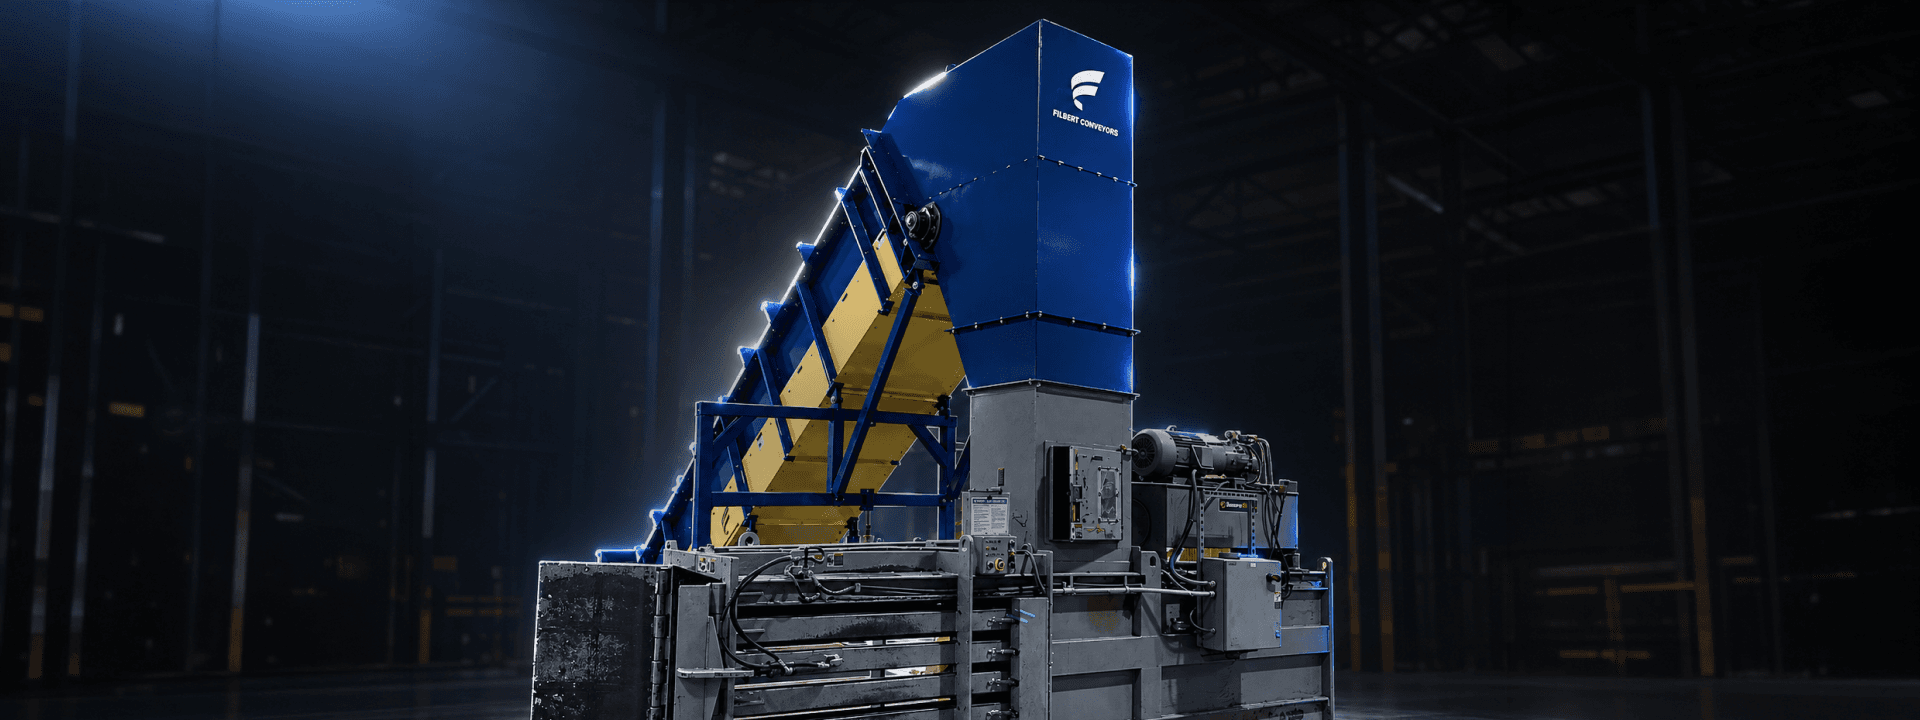
Conveyors move material from one location to another. They operate on a simple principle: a belt turns and transports materials that ride upon it. An electric motor powers the conveyor belt through a drive pulley or a chain system.
Conveyors save time and reduce manual labor costs in assembly lines, recycling efforts, and other applications.

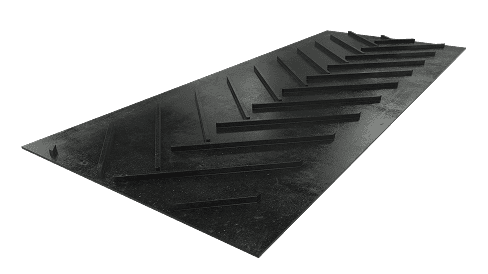
Belt conveyors are the most common type of conveyor. They utilize a continuous loop of flexible belting to transport materials.
The conveyor belt is stretched between two or more pulleys, one of which is the drive pulley, powered by the motor. As the motor rotates the drive pulley, it creates tension on the belt, causing it to move and carry items along the conveyor frame.

Flat idler conveyors utilize Idlers and rollers, positioned along the length of the frame, to support the belt and smooth belt movement. Flat belt conveyors are commonly used in manufacturing and distribution facilities.
Trough idler conveyors feature a belt supported by unpowered idlers, but the idlers have angled wings that bend the belt into a trough to collect and control loose materials.
Slider bed conveyors take a different approach. The belt is pulled over a flat metal bed instead of idlers, offering a quieter and more precise conveying solution for smaller, lighter materials.
Conveyor belts can be highly customized to suit different industries and applications. Steel belts, cleated belts, and corrugated sidewall belts are some of the common types of conveyor belts found in industrial settings. Belts can also be customized through various cleat patterns molded or adhered to the belt, such as chevrons, herringbones, and bullhorns.
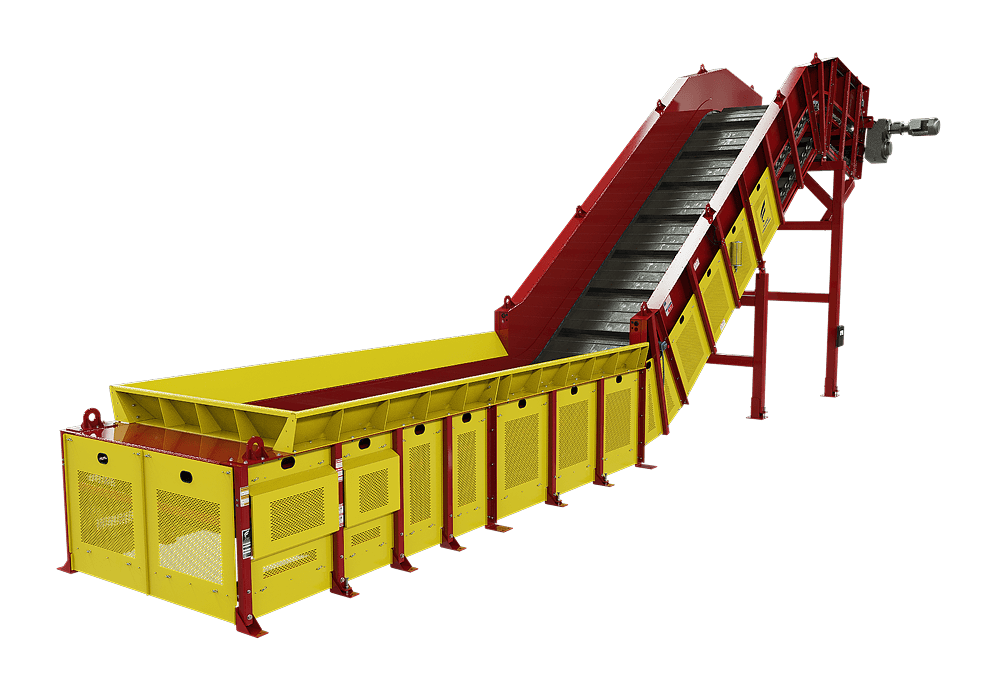
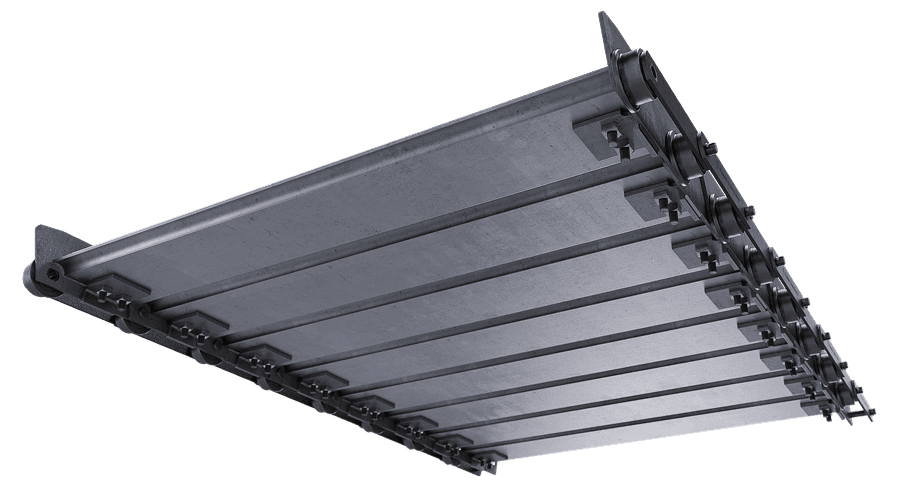
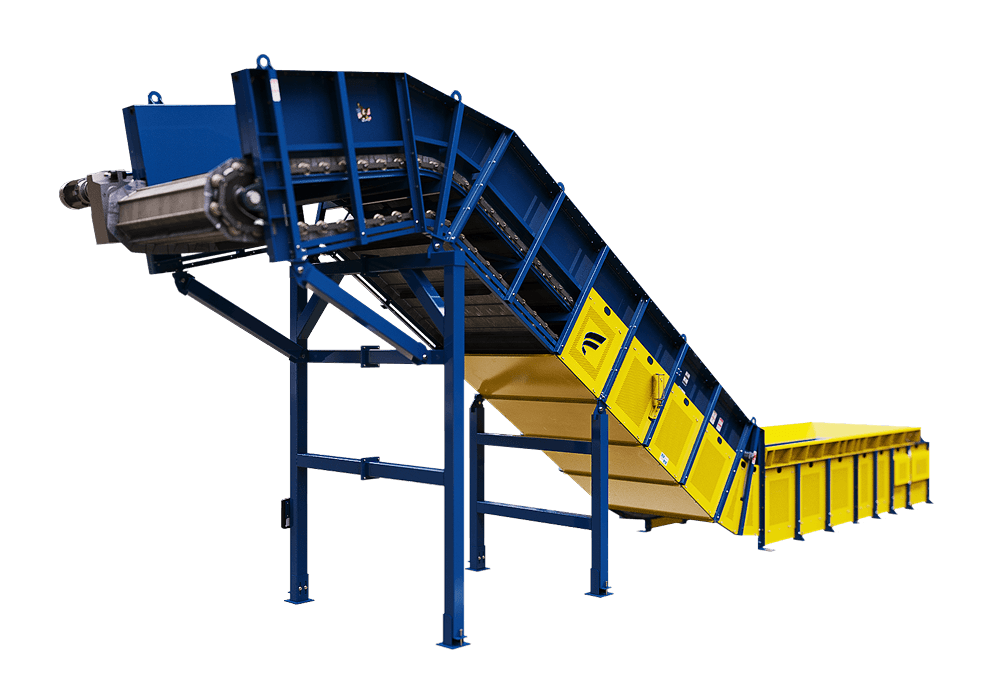
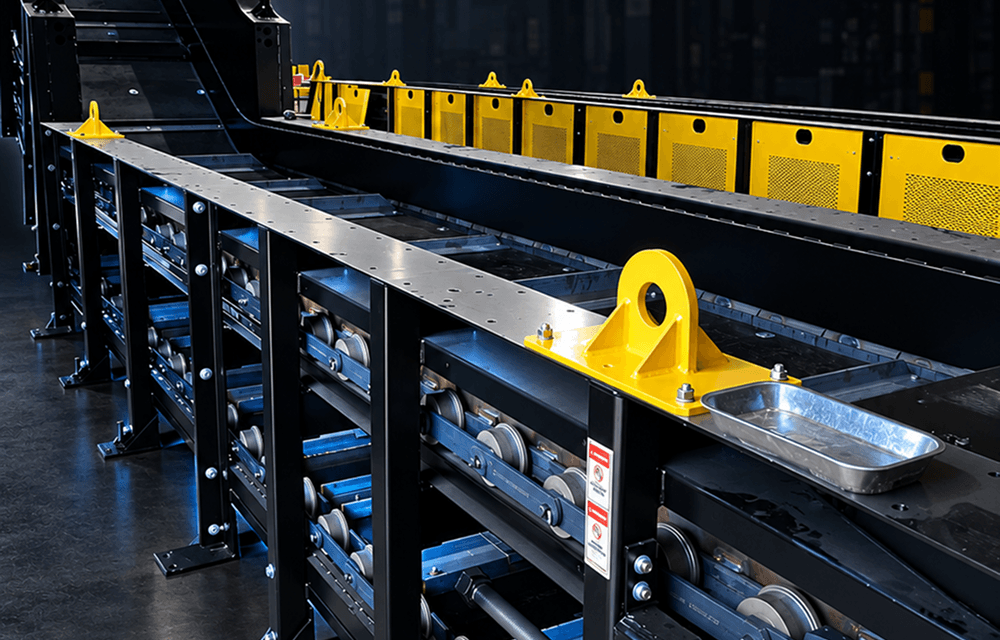
Roller chain conveyors employ a series of sprockets and a chain that moves in an endless loop. The motor transfers power to a drive sprocket, which engages the chain with its teeth to initiate movement.
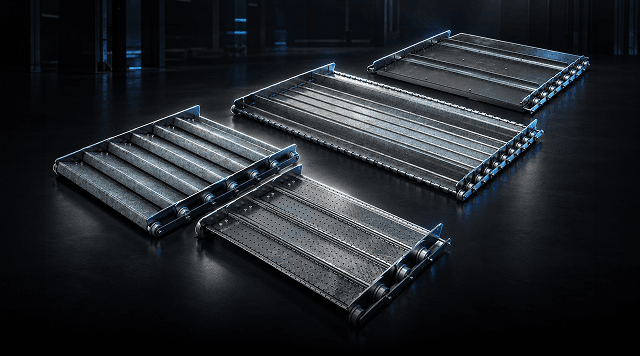
This chain propels a steel (or rubber-steel combination) belt. Roller chain belts excel at moving heavy items, abrasive materials, and granular materials with precision and durability.
Roller chain conveyors offer a simple yet effective solution for sorting, transporting, and feeding a wide range of materials in manufacturing, material recovery, and distribution centers.
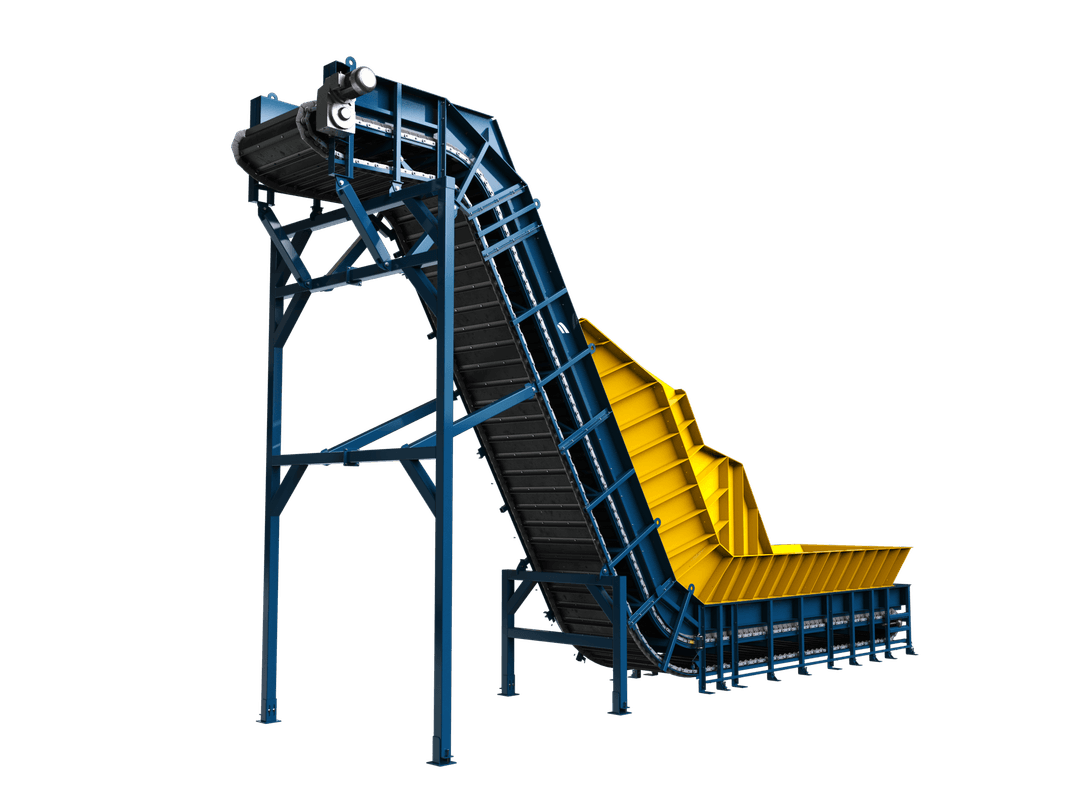
Use a belt made of a closed loop of interlocking plates. They excel at handling abrasive and heavy materials.
Found in many scrap yards, car shredder infeed conveyors operate at an incline and feed cars and scrap metal into industrial shredders.
Belting options for chain-fed systems are highly customizable. Options such as z-pan, rubber combination, apron, and hinged steel belts allow roller chain conveyors to be adapted to many different heavy-duty industrial applications.
Conveyors dramatically improve material handling operations. They streamline the production process, optimize warehouse operations, and boost overall efficiency. Here are some of the key advantages of implementing conveyor systems:
By harnessing the power of automation, conveyors drive efficiency, safety, and profitability for businesses.
Need a custom conveyor solution? We can help you design a conveyor to suit your needs. All Fluent conveyors are engineered and manufactured in the USA to the most stringent tolerances.

Goodyear, Flexco belt options resistant to rips, tears, and impacts

Baldor, Leeson, Toshiba TEFC motors selected for 24/7 operation

All systems fabricated by certified welders for structural integrity.

Formed using heavy duty steel plate, rectangular tubing, and structural channel

Precision components such as cold-rolled steel shafts and flame-hardened sprockets

All hardware is grade 8 for maximum strength

Extensively tested and inspected prior to shipment

3/16" and 1/4" thick structural steel frames to prevent flexing

25-35 pound rail track to withstand heavy loads

Designed for simple maintenance access and component serviceability

Dodge, Nord, SEW drives matched to application torque

ASTM A36 steel for fabrication per structural code

Premium bearings sized for L10 life ratings, made in USA

Painted with industrial-grade powder coating for durability
Made from durable materials, our conveyors deliver exceptional strength and longevity for recycling, waste management, and other demanding industries. Whether you need a roller chain conveyor, a trough idler conveyor, or any other conveyor system, contact Fluent and tell us what you need. We will build you a custom material handling system—and you can even pick your own color.